How Sharpen Bandsaw Blade: Practical Workshop Guide for 2026
Learn How Sharpen Bandsaw Blade step by step to eliminate blade drift, restore tooth set, and extend cutting life across workshop saws in October 2026.
 By Andrew McKean
Updated October 2, 2026
Dull bandsaw teeth can quickly ruin a project by producing barreled cuts, burning dense hardwoods, and wandering off scribe lines under normal feed pressure. Learning How Sharpen Bandsaw Blade allows woodworkers and sawyers to restore clean cutting performance without immediately discarding costly bands. Instead of forcing dull teeth through stock and overheating the motor, establishing a consistent sharpening routine restores the cutting face, clears chip evacuation pathways in the gullet, and preserves true tracking across the wheel tires. Proper blade reconditioning pairs naturally with other workshop milling tasks like sawing planks of wood to ensure every board comes off the machine flat and true.
Maintaining a sharp band also reduces the excessive feed pressure that deflects steel bands and overworks stationary motor assemblies. Routine tooth touch-ups extend overall blade longevity, preserve the engineered tooth set, and minimize lateral blade wander along the rip fence. Whether you are servicing wide bandsaw mill blades or touching up general-purpose shop bands, understanding tooth geometry and abrasive methods ensures dependable cut quality. Disconnecting power before servicing and following structured alignment practices keeps the entire sawing system operating with precision and safety.
| Award | Product | TGH Score About TGH ScoreThe TGH Score is our own rating from 0 to 10, based on performance, design and build, ease of use, and value. It reflects independent research and is never influenced by manufacturers, retailers, or affiliate commissions. Learn more › | |
|---|---|---|---|
| Best Overall |
LENOX Tools Portable Band Saw Blades
|
7.8/10 | Buy |
| Best Value |
 Wood-Mizer 158" Sawmill Bandsaw Blades 5-Pack |
7.8/10 | Buy |
The Mechanics of Sharpening and Reconditioning Bandsaw Blades
Every bandsaw blade eventually loses its keen cutting edge, causing increased friction, scorch marks, and drifting cuts. Restoring a dull blade requires grinding or filing the tooth faces while preserving the original tooth rake angle and gullet profile. Before attempting any sharpening operation, you must determine whether the blade metallurgy, tooth pitch, and overall band condition justify the labor. Wide carbon steel resaw bands and large sawmill blades offer ample steel for repeated grinding, whereas fine-pitch metal cutting bands are often run to exhaustion and replaced.
Anatomy of a Dull Tooth and Feasibility Assessment
A sharp bandsaw tooth relies on two crisp planes meeting at a defined cutting edge: the tooth face and the tooth back. As cutting friction wears the tip, the leading edge rounds over, forcing the operator to push stock harder to maintain forward progress. This rounded tip cannot sever wood fibers cleanly, creating excess heat and packing sawdust into the tooth gullet. Inspecting the edge under strong shop lighting reveals wear immediately because a rounded tooth tip reflects bright highlights, while a sharp edge remains dark.
Beyond edge dullness, examine the blade body for micro-cracks in the gullets and excessive fatigue around the weld joint. When a blade has run through repeated flex cycles over wheels, metal fatigue hardens the steel band and creates tiny stress fissures. Sharpening the teeth will not rescue a band that has developed gullet fractures, as the blade will snap under working tension. Coarse blades with fewer than 6 TPI are the best candidates for shop reconditioning because their large teeth accommodate sharpening tools easily.
Blade Metallurgy and Abrasive Media Compatibility
The steel composition of your bandsaw blade directly dictates the abrasive or cutting tool required for sharpening. Standard carbon steel blades feature relatively soft backing steel with hardened tooth tips that respond well to standard mill files and aluminum oxide stones. These economical blades file quickly, but their edge retention is lower when cutting dense hardwoods. Specialized alloys, however, require aggressive abrasive media to remove metal without generating damaging surface heat.
High-alloy bands, such as Wood-Mizer DoubleHard blades, incorporate specialized alloy steel engineered for extended cutting life between sharpenings. These bands are formulated to be resharpened using cubic boron nitride (CBN) grinding wheels that maintain precise tooth profiles without glazing. Cubic boron nitride grains resist thermal breakdown and cut cooler than traditional wheels, preventing metallurgical softening. Attempting to sharpen high-alloy steel with standard files will merely dull the file without restoring the edge.
Bi-metal blades introduce an even tougher challenge because their tooth tips consist of high-speed steel welded to a flexible spring-steel backing. The extreme hardness of high-speed steel resists standard files and requires diamond or CBN abrasives for effective touch-ups. For fabricators comparing cut-off methods, using dedicated metal cut-off machinery highlights how different tool steels handle abrasive wear and heat dissipation. Matching your abrasive directly to blade metallurgy prevents ruined tooling and preserves the original tooth geometry.
Resharpening Large Sawmill Bands with CBN Profile Wheels
Sawmill operations require repeatable, high-precision grinding systems to keep wide bands tracking and cutting true across timber logs. Bands such as the Wood-Mizer 158-inch DoubleHard blades utilize a 10-degree hook angle with 7/8-inch tooth spacing to clear sawdust rapidly. Maintaining this 10-degree face angle and sweeping gullet radius prevents sawdust packing and overheating, which automated grinding machines accomplish using a profile-matched CBN wheel.
The profile wheel grinds the face, passes smoothly through the gullet, and finishes the tooth back in a single fluid stroke. Continuous flood coolant must wash over the grinding zone to flush steel swarf and suppress thermal buildup. Removing merely 0.003 to 0.005 inches of steel per pass restores a sharp cutting edge without wasting valuable tooth material.
Automated indexers advance the blade tooth by tooth using a push dog that registers against each tooth face. The operator must adjust the stroke carefully so the grinding wheel contacts each tooth with identical downward pressure. Consistent indexing guarantees uniform tooth heights across the loop, preventing taller teeth from shouldering all the cutting load.
Freehand Rotary Tool Sharpening for Workshop Bands
Woodworkers operating stationary vertical bandsaws can sharpen blades directly on the machine using a high-speed rotary tool equipped with a diamond burr. Disconnect the bandsaw from its electrical source before opening wheel cabinet doors or touching the blade. Select a cylindrical diamond burr whose diameter matches the blade gullet curvature, typically 1/8 inch to 3/16 inch for general-purpose blades. Mount a work light directly above the upper guide area to provide clear visibility of the tooth faces.
Hold the rotary tool firmly with both hands and match the burr angle precisely to the factory face angle of the tooth. Touch the spinning diamond burr against the tooth face with light, momentary pressure, holding contact for less than one second. The goal is simply to polish away the rounded micro-edge while removing minimal metal. Avoid grinding deep into the gullet bottom during this touch-up to prevent creating stress risers.
Mark your starting tooth with a felt-tip marker on the outer band surface to track your progress around the blade loop. Advance the blade upward by hand against the normal direction of travel, keeping your fingers clear of sharp teeth. Grind only the face of each tooth consecutively until you reach your initial mark. Working systematically around the band prevents skipping teeth and ensures that every cutting edge receives identical contact.
Manual Hand Filing for Low-Pitch Carbon Blades
Manual filing provides exceptional control for coarse resaw blades with 2 to 4 TPI made from standard carbon steel. Clamp the bandsaw blade securely between two hardwood backing strips in a bench vise to dampen vibration and support the thin band. A sharp 6-inch smooth-cut mill bastard file addresses individual tooth faces with high precision. Because standard steel files cut on the forward stroke only, lift the file completely off the tooth on the return stroke.
Maintain a perpendicular stroke relative to the side of the blade band to keep the cutting face square. Count your strokes on each tooth, applying two or three firm passes per face to achieve uniform metal removal. If the tooth has a positive hook angle, tilt the file to match that inward rake rather than filing the face flat. Consistent hand pressure is vital because filing teeth unevenly produces erratic cutting forces during operation.
Once you finish dressing the tooth faces, inspect the back edge of each tooth for any raised wire burrs. A quick, light pass with a fine diamond hone flat against the blade side cleans away these burrs without disturbing tooth set. Clean tooth edges reduce cutting drag and prevent pitch buildup when resawing woods like pine or cherry. Taking time to file methodically creates cut finishes comparable to dedicated rip cuts on portable table saws for cabinet making without requiring automated tooling.
Understanding and Restoring Tooth Set
Sharpening the face of a tooth restores sharpness, but it does nothing to correct a blade that binds due to collapsed tooth set. Tooth set refers to the intentional alternating bend of tooth tips away from the blade centerline, creating a kerf wider than the blade steel. This clearance allows the blade body to pass freely through the cut without rubbing against kerf walls. When cutting abrasive hardwoods, the outer tooth corners wear down, narrowing the kerf and causing friction, smoke, and severe drift.
Checking tooth set requires a dial indicator gauge or a machinist caliper to measure total kerf width. For standard woodworking bands, the set typically extends 0.005 to 0.015 inches per side beyond the band thickness, depending on blade width. If the teeth have lost their offset, sharpening alone will leave you with a blade that still stalls in thick cuts. You must mechanically bend the teeth outward using a commercial tooth setter or manual setting pliers designed for bandsaws.
A tooth setter uses hardened anvils to push alternating teeth to the left and right in a precise pattern, often leaving an unset raker tooth between pairs. Both sides of the blade must receive identical set deflection to maintain balanced cutting resistance. If the left teeth extend further than the right teeth, the blade will pull relentlessly toward the left side during every cut. Symmetrical tooth set is just as critical as sharp tips for producing straight, reliable cuts along a fence.
Practical Realities of Fine-Pitch and Portable Blades
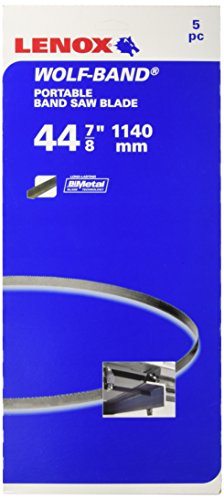
While coarse resaw bands and large sawmill loops justify the labor of sharpening, fine-pitch bands present a different economic equation. Compact blades, like the Lenox Tools Portable Band Saw Blades measuring 44-7/8 inches by 1/2 inch with 14 TPI, contain hundreds of diminutive teeth. The bi-metal high-speed steel cutting edge on these portable blades resists wear effectively, but grinding teeth spaced mere fractions of an inch apart by hand is impractical. Attempting to sharpen a 14 TPI band freehand almost inevitably rounds over adjacent teeth and destroys tooth spacing.
Portable metal-cutting bandsaws subject narrow blades to extreme twisting and tight radius bends around small-diameter drive wheels. By the time the teeth lose their initial edge, the underlying steel backing has endured substantial bending fatigue. Investing workshop hours attempting to dress bi-metal teeth on a budget replacement pack rarely yields a durable cutting edge. For narrow contour blades and fine-pitch metal-cutting bands, replacing the blade represents a far more practical use of workshop resources.
Preventing Critical Grinding and Thermal Errors
The most common mistake when sharpening bandsaw blades is applying excessive pressure and overheating the tooth tip. When steel turns a dark blue or straw color during grinding, friction has pushed temperatures beyond the critical transformation point, drawing out the factory temper. An annealed tooth becomes soft and dulls within a few inches of cutting, defeating the entire purpose of the sharpening effort. Use light, fluttering grinding passes and allow the metal to cool between strokes, applying grinding fluid if your machine supports liquid delivery.
Another dangerous hazard involves creating sharp gouges or square corners at the bottom of the tooth gullet. A properly engineered bandsaw blade features a continuous, smooth radius in the gullet to distribute flexural stress evenly as the band cycles over the wheels. If a sharp grinding wheel nicks the gullet bottom, that small notch acts as a stress concentration point where bending forces focus. Within hours of running under high tension, a stress fracture will propagate outward from that notch, causing the band to snap abruptly.
Bandsaw Reinstallation and Post-Sharpening Calibration
Reinstalling the sharpened band requires a systematic mechanical setup to ensure accurate, drift-free tracking. Verify the machine is disconnected from electrical power before mounting the band over the upper and lower wheels. Back off all upper and lower guide blocks and rear thrust bearings completely so they cannot touch the blade during initial alignment. Apply baseline tension and spin the upper wheel by hand, ensuring the deepest part of the tooth gullet rides directly over the apex of crowned wheel tires.
Once tracking is centered, tune blade tension using the flutter method rather than relying on built-in spring indicator scales. Close the cabinet doors, start the saw, and slowly back off tension until the blade flutters laterally between the wheels. Turn the tension knob inward until the flutter ceases, then add another quarter to half turn of tension to establish baseline beam strength. This procedure provides adequate beam rigidity for resawing while avoiding excessive strain on bearings and wheel shafts.
With tension set, bring the side guide blocks or roller bearings toward the blade, leaving a clearance of 0.002 to 0.004 inches on each side. A single slip of standard 20-pound copy paper placed between the guide and blade serves as an ideal feeler gauge. Position the front edge of the guide blocks 1/16 to 1/8 inch behind the tooth gullets to protect the tooth set. Adjust the rear thrust bearings so they sit roughly 1/32 inch behind the blade spine, spinning only when cutting pressure pushes the blade backward.
Before beginning your cut, lower the upper telescoping blade guard post until it rests 1/8 to 1/4 inch above the workpiece surface. Never allow hands or fingers to operate within 3 inches of the exposed blade line, using push sticks or push blocks to feed stock. Ensure your blade tooth pitch maintains at least 3 teeth in continuous contact with the material thickness to prevent tooth stripping. Making a test cut in scrap lumber confirms your freshly sharpened blade cuts square and straight.
About the author
Andrew McKean is an experienced outdoor journalist and optics specialist with extensive experience evaluating binoculars, spotting scopes, and other outdoor optical equipment. His work combines practical field testing with detailed technical analysis, helping readers understand optical performance, durability, and the features that matter when comparing equipment.